Press Room

Press Clipping / Mar 19, 2020

Stepping up to the hand sanitizer shortage

Chemical companies, breweries, and perfumeries take to making and donating a vital commodity in short supply

Production of Hand Sanitizers | Hovione

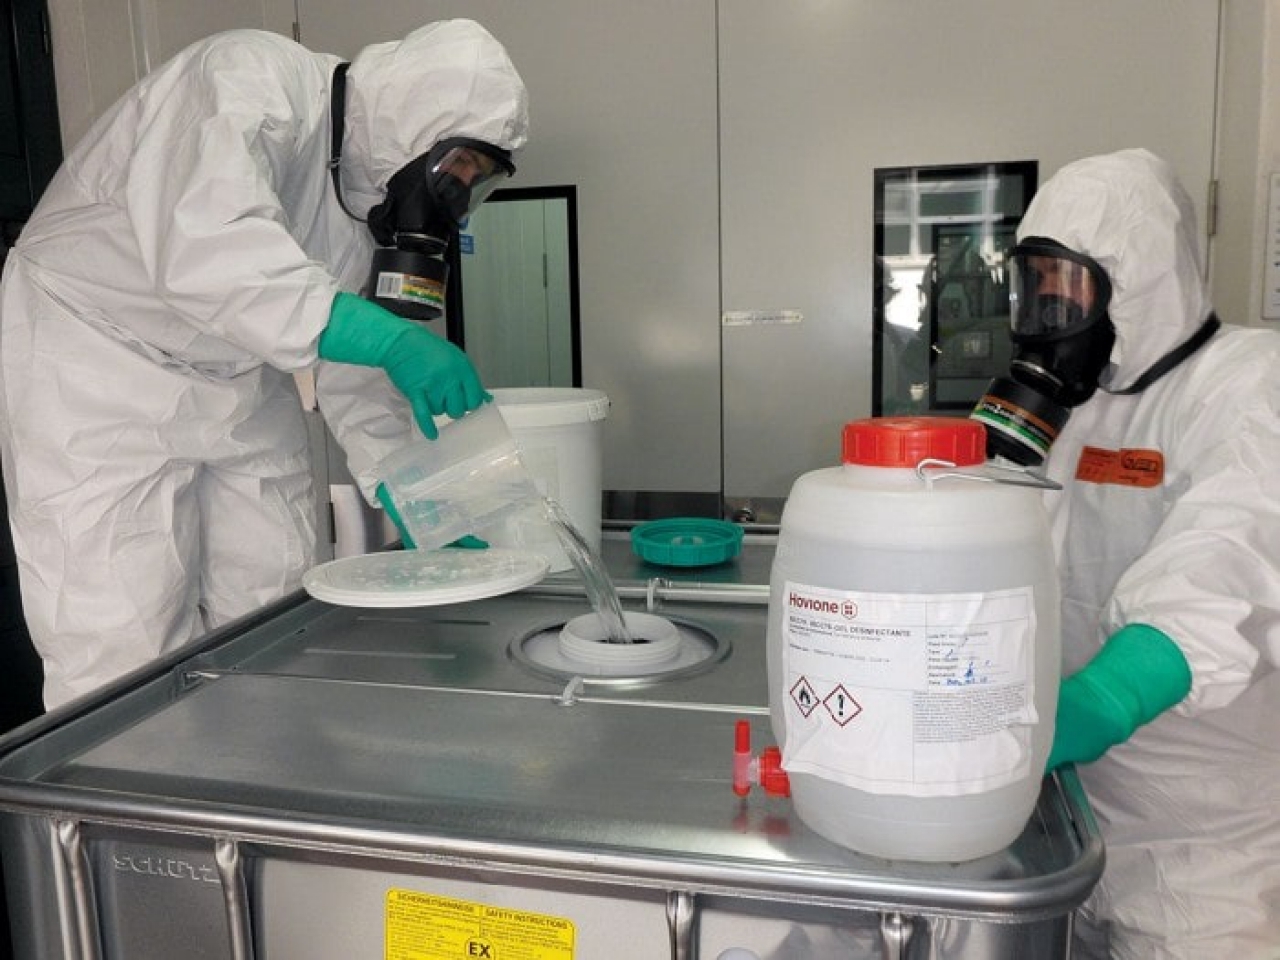
About 6 weeks ago, the pharmaceutical chemical maker Hovione ran out of disinfectant gel at its plant in Macau. “So the guys just used their heads and started manufacturing it themselves,” CEO Guy Villax says.

Hovione is one of a number of chemical, distilling, and other companies that are starting or increasing production of hand sanitizers and sanitizer ingredients needed during the coronavirus pandemic. Some are already in the sanitizer business. Others, like Hovione, jumped in during a time of need.

Impressed by the initiative in Macau, Villax put staff at the company’s plant in Loures, Portugal, to work making alcohol-based sanitizer at metric-ton scale. Hovione is distributing it to hospitals, other health-care facilities, and municipalities in solution and gel formulations.

Hovione has enlisted a dedicated production line in Loures staffed by a team of about 30 workers. The company is using a formula available from the World Health Organization involving mainly ethanol or isopropyl alcohol and glycerin. Production volume was expected to reach 5 metric tons (t) during the week of March 16 and as much as 30 t by the following week.

“At the moment we have hospitals asking us for 6 to 10 t, small entities asking for 100 L,” says Filipe Neves, pilot plant operations director, who is overseeing the project for Hovione in Loures.

In Germany, the big chemical maker BASF says it is preparing to manufacture hand sanitizer at its headquarters complex in Ludwigshafen, where it makes raw materials for sanitizers. The company plans to distribute the product to area hospitals.

UK-based Psychopomp & Circumstance Distillery, which normally distills gins and rums, is using its still to make sanitizing hand gel that it is giving away. Consumers can top up their own refillable bottles at the firm’s still in Bristol and leave a donation for a local children’s hospital.

At the moment we have hospitals asking us for 6 to 10 t small entities asking 100 L.

Filipe Neves, pilot plant operations director, Hovione

The company started out mixing its alcohol with aloe vera gel but has since switched to glycerin. “We are making as much of it as we can without going bankrupt,” Psychopomp cofounder Liam Hirt says.

Ireland-based Listoke Distillery has also switched production from gins to alcohol for hand gels, as have Taiwan Tobacco and Liquor and a number of small US distillers.

The flavor and fragrance producer Firmenich has shifted production at its La Plaine, Switzerland, facility to disinfectant solution. LVMH, the parent company of luxury goods maker Luis Vuitton, has switched three of its perfume facilities in France to making “substantial quantities” of alcohol-based hand sanitizer. The firm is giving the product to the French health authorities for free.

Specialty chemical manufacturers in the business of making sanitizing and disinfecting chemicals are boosting production. Lanxess is significantly increasing output of its Vikron sanitizer in Sudbury, England—introducing a second shift. The company recently donated a metric ton of disinfectant to hospitals in Wuhan, China, the epicenter of the virus outbreak, and to nearby cities.

And Gelest has significantly ramped up production of its Biosafe antimicrobial agent at its facility in Morrisville, Pennsylvania. Based on a silane quaternary ammonium salts, Biosafe punctures the cell membranes of microbes, destroying them on contact. Applications include formulations used by food service workers.

Biosafe is also the microbe-killing ingredient in a laundry additive called Certainty Smartboost, from the uniform company Careismatic Brands, which is sold primarily to health-care workers in specialty stores near hospitals. Workers use the treatment on their hospital scrubs or uniforms because it provides antimicrobial protection after they are washed.

Drums of Biosafe are “flying off the shelves” to formulators of cleaning products, including nonwoven wipes, according to Gelest CEO Ken Gayer. “We’re now also seeing direct orders from hospitals that want cases and cases of this material and are giving it to staff members.”

Read the article at C&EN website


Also in the Press Room

See All

Key Takeaways Commissioning a US-based ConsiGma CDC Flex line enables end-to-end spray drying-to-tablet manufacture within a single site and quality system, reducing comparability and technology-transfer burdens. Elimination of conventional scale-up is enabled by using the same equipment from early development through commercial supply, minimizing engineering runs and conserving scarce API. Operational flexibility spans batch or continuous modes and 1–200 kg/h throughput, with scale adjustment achieved by switching continuous blenders rather than replatforming processes. High-containment design to 1 µg/m³ expands suitability for highly potent oral solid-dose programs while maintaining integrated development-to-commercial workflows. Regulatory momentum for continuous manufacturing is supported by ICH Q13 harmonization, increasing FDA approvals, and platforms leveraging inline PAT and automated control suites for real-time quality assurance. Hovione announced on Oct. 5, 2026, that it will commission the ConsiGma CDC Flex, a next-generation continuous direct compression tableting platform jointly developed with GEA. The investment is designed to link amorphous solid dispersion manufacturing via spray drying with commercial tablet production at a single US site operating under one quality system. The line will run in either continuous or batch mode at throughputs from 1 to 200 kg/h. Formulation development can begin with as little as 1.5 kg of material, and the same equipment can then support everything from very small clinical batches to large commercial runs, enabled by a design that allows the system to switch between continuous blenders of different sizes. The installation will also be contained to 1 µg/m³ to accommodate highly potent compounds. "Hovione will be the first company in the world to offer the ConsiGma® CDC Flex, bringing this next-generation technology with unprecedented flexibility, simplicity and cost-efficiency in continuous tableting," said Marco Gil and António Almeida, co-CEOs, Hovione, said in a press release. "This investment also advances our strategy of building integrated capabilities close to customers in key markets. By adding this new line at East Windsor, we are broadening access to this technology in the U.S. and giving customers a more direct and accelerated path for developing and commercializing complex oral medicines." What Does a Single Development-To-Commercial Line Change? For formulators and process engineers, the most consequential claim is the removal of traditional scale-up. Moving a process from development equipment to commercial equipment typically requires engineering runs, bridging work, and consumption of scarce API, all of which weigh heavily on early programs with limited material. "Installing the CDC Flex at 89 Twin Rivers makes continuous tableting part of an integrated US development and manufacturing workflow," said David Basile, Vice President of Technical Operations, Hovione, in the press release. "Customers can move from formulation and particle engineering to commercial tablets with one Hovione team and one quality system, eliminating traditional scale-up while gaining greater production flexibility, process control and supply continuity." Co-locating spray drying and tableting is also significant because amorphous solid dispersions remain a primary solubility-enhancement route for poorly soluble molecules, and transferring intermediates between sites or vendors adds technology transfer and comparability burdens. The new line builds on the company's earlier US expansion; Hovione recently completed a $100 million investment to bolster US capacity in particle design, amorphous solid dispersions via spray drying, and batch and continuous tableting. How Is the Regulatory Environment Shaping Continuous Tableting Adoption? The company points to the 2022 adoption of ICH Q13, which provides harmonized guidance for continuous manufacturing of drug substances and drug products across the US, Europe, and Japan. Hovione reports that, as of 2024, FDA alone had approved 17 products manufactured under the guidance. Speaking on ICH Q13, FDA's Kelley Burridge, PhD, "Perceived barriers to continuous manufacturing have been falling one by one," and noted an FDA publication showing faster approval times for products with continuous manufacturing elements than for comparable batch products. The platform incorporates inline process analytical technology and automated controls for real-time quality monitoring, along with SimpleCT, an automation and control suite intended to support a single process from development through commercial supply. For sponsors weighing supply resilience and regional sourcing, the East Windsor installation extends a capability that Hovione says only it currently offers as a contract development and manufacturing organization.   Read the full article at PharmTech.com  

Press Clipping

Can Continuous Tableting End Scale-Up for Complex Oral Drugs?

Oct 05, 2026

The company is building out more than 200,000 square feet of space in New Jersey. In April, Contract Pharma had the opportunity to tour Hovione’s expanded manufacturing facility in East Windsor, NJ. The company is planning a formal ribbon-cutting this fall; before that, we got an inside look at some new features. Having established United States operations in 2002, Hovione now has more than 200,000 square feet of space in New Jersey. This will be developed into a large, integrated campus in the next five to ten years. Overall, the company’s recent NJ expansion, which began in 2025, has tripled its total spray-drying capacity in the U.S. Future Facility Upgrades A 125,000-square-foot greenfield acquired by Hovione at the East Windsor campus will eventually be a large-scale production site. This includes enhanced quality control and R&D capabilities. Together, all this adds to Hovione’s stable of manufacturing sites, R&D centers, and other offices spread across three continents. Key to the expansion is a targeted reduction of Hovione’s carbon footprint by 40% by the year 2030. Part of this goal is embracing new and/or changing solvent types to help meet sustainability standards. Additionally, the company says automation that has been put in place at its Portugal site will be replicated in NJ. Hovione Aligns NJ Operations At the Drug, Chemical & Associated Technologies Association (DCAT) Week in New York in March, Contract Pharma met with Hovione. There, David Basile, Vice President of Technical Operations—Americas, further illustrated the New Jersey expansion. “Hovione aims to build an equivalent manufacturing network, where clients can go to any site across the globe,” Basile said. “The design of the facility has been well-thought through with material flows [and] gravity-fed processes. It’s scalable. We call each one of these building segments a finger. You can copy and paste these fingers, and they are built to house both spray drying and drug product assets.” Ultimately, with these moves and a strategic partnership model, Hovione aims to provide customers an opportunity to co-invest and access the company’s proprietary knowledge and assets to accelerate programs and create long-term value. Read the full article at ContractPharma.com    

Press Clipping

Hovione Planning Ribbon-Cutting at NJ Facility – A Behind-the-Scenes Preview

Jul 31, 2026